


日本語
- English
- Portugal
- 日本語
- Русский
- SaudiArabia
- 한국어
- Português
- ภาษาไทย
- Español
- Tiếng Việt


問い合わせ


5 インチ (127mm) x 4mm ERW チューブミル
溶接前にチューブを成形部の従動ローラと従動ローラの組を通過させて丸く成形し、溶接部で高周波誘導溶接法を用いてチューブを縦方向に溶接し、外側のビードを除去してスクラップ状に成形します。しごき加工を経てチューブを冷却セクションを通過する サイジングセクションでチューブを指定サイズに成形し、所定の形状に加工する サイジング後、チューブを所定のサイズに切断し、所定の形状に加工する
LIST OF EQUIPMENT AND SCOPE OF SUPPLY
Equipment | Quantity |
Entry Section ▪Double mandrel Uncoiler ▪Shear & welder, with TIG welder ▪Horizontal strip accumulator |
1No. 1No. 1No. |
Forming, welding, cooling and sizing section ▪Forming mill with drive unit ▪welding mill ▪Solid state H.F. induction welder ▪Cooling trough ▪Sizing mill with drive unit |
1set 1No. 1No. 1No. 1set |
Cutting and Delivery Section ▪Friction saw cut-off ▪Driven roller run out table ,Inspection table & Collectors |
1No. 1No. |
Auxiliary equipment ▪Roll coolant system(cooling tower) ▪Centralized lubrication system ▪Hydraulic. Power Unit ▪Coolant liquid purify device |
1No.. 2Nos. 2Nos. 1No |
Electrical Equipment ▪PCC Panel ▪AC/DC Motors ▪Drive Panels ▪MCC Panels ▪PLC(Fitted in one drive panel) ▪Control Desks |
1No As specified 3Nos. 1No. 1No. 3Nos. |
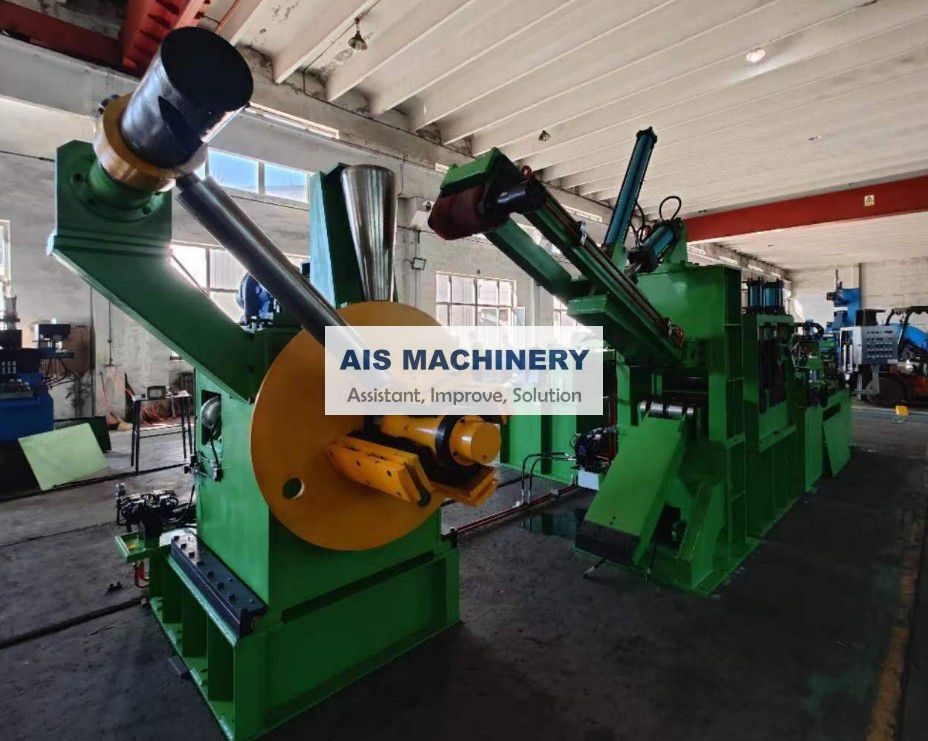
提案されたチューブミルは、高周波誘導溶接 (HFIW) 炭素鋼鋼管の製造ラインに設置された装置を組み合わせたもので、円形の炭素鋼ストリップの冷間成形、縦方向の溶接、サイジング、指定された鋼管への変換が含まれるプロセスです。形状を整えて所定の長さにカットします。
完全なラインは 3 つのセクションに分かれています:
▪ エントリーセクション
▪ 成形、溶接、冷却、サイジングセクション
▪ 切断搬送部
コイル状の原料(鋼帯)を解きほぐし、入口部の設備を経て成形部に供給します 入口部では鋼板接合・集積装置によりチューブミルを連続運転することができます 管は円形に通過して成形されます溶接前に成形部の従動ローラと従動ローラの組を通過させ、溶接部で高周波誘導溶接法を用いてチューブを縦方向に溶接する 外側のビードを除去してスクラップ状に成形する 溶接シームをしごいてチューブを通過させる冷却セクション サイジングセクションでは、チューブを指定のサイズに成形し、指定の形状に変換します サイジング後、チューブを指定のサイズに切断し、指定の形状に変換します サイジング後、フライング切断装置によりチューブを指定の長さに切断し、納品しますランナウトコンベアを通過しながら回収中。

1. BASIC DESIGN DATA
Design of the proposed line is based on following specification:
▪ Raw Material Specification
Raw Material Feeding | CR bright tube with oiled, Galvanized steel, HR coil |
Material Tensile Strength | Max 517MPa (75,000 psi max) |
Material Yield Strength | Max 460MPa (67,000 psi max) |
Coil OD | 1200mm to 2000mm |
Coil ID | 508mm&610mm (customer order) |
Coil Weight | Max 7000 kg |
Strip Width | Min 80mm, Max400mm |
Strip Thickness | Min2.0mm Max4.0mm |
▪ Production Range
Type of production | ▪Round Tubes ▪Square and Rectangular Hollow Sections |
Round Tube OD | Min 25.4mm, Max 127mm |
Round Tube Thickness | Min 2.0mm, Max 4.0mm |
Square Hollow Section | Min 20x20mm, Max 100x100mm |
Rectangular Hollow Section | Min 30x20mm, Max 120X80mm |
Square and rectangle Tube Thickness | Min2.0mm, Max 4.0mm |
Tube Cut Length | Min 6 meter, Max 12 meter |

▪ Line Specification
Line speed | Max 50m/min Min 10m/min |
Direction of Operation (To be confirmed by buyer) | Left → Right or Right → Left |
Welding Method | High Frequency Induction Welding |
Total Electric installed capacity | 800kw |
Line area | Approx. 70x8.0 meter (length x width) |


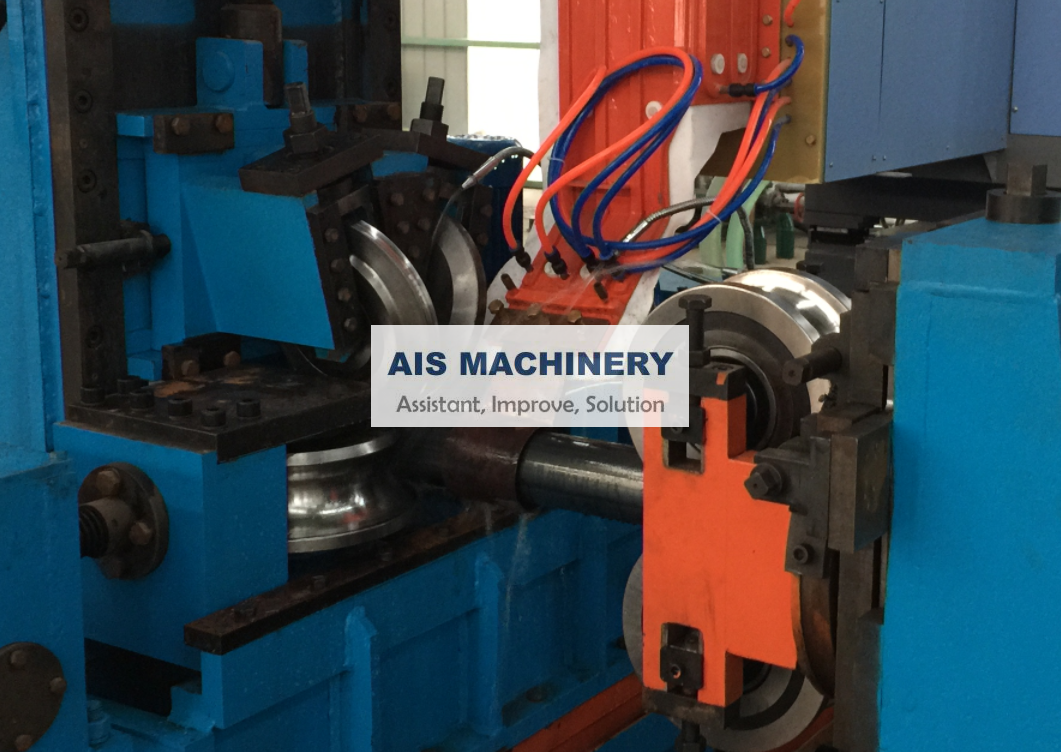
Forming Section
轴材质Shaft material: | 40Cr, HF tempering quenching |
减速箱齿轮Material of bevel gear: | 20CrMnTi |
水平辊架Driven stand | 7 sets |
立辊架Idle stand | 8 sets |
减速箱Gear box | 7 sets |

Sizing Section
轴材质Shaft material: | 40Cr,HF tempering quenching |
减速箱齿轮Material of bevel gear: | 20CrMnTi |
水平辊架Driven stand | 5 sets |
立辊架Idle stand | 5 sets |
减速箱Gear box | 5 sets |


Why Choose Us?
Leading Technology, Reliable Quality, Excellent Service!
Optimized Design, High quality material select!
Heat treatment process guarantee!
Spiral bevel gear, drum gear coupling and carburization.
Gear teeth quenching.
Driven system stable, efficient and wearable with lower noise.
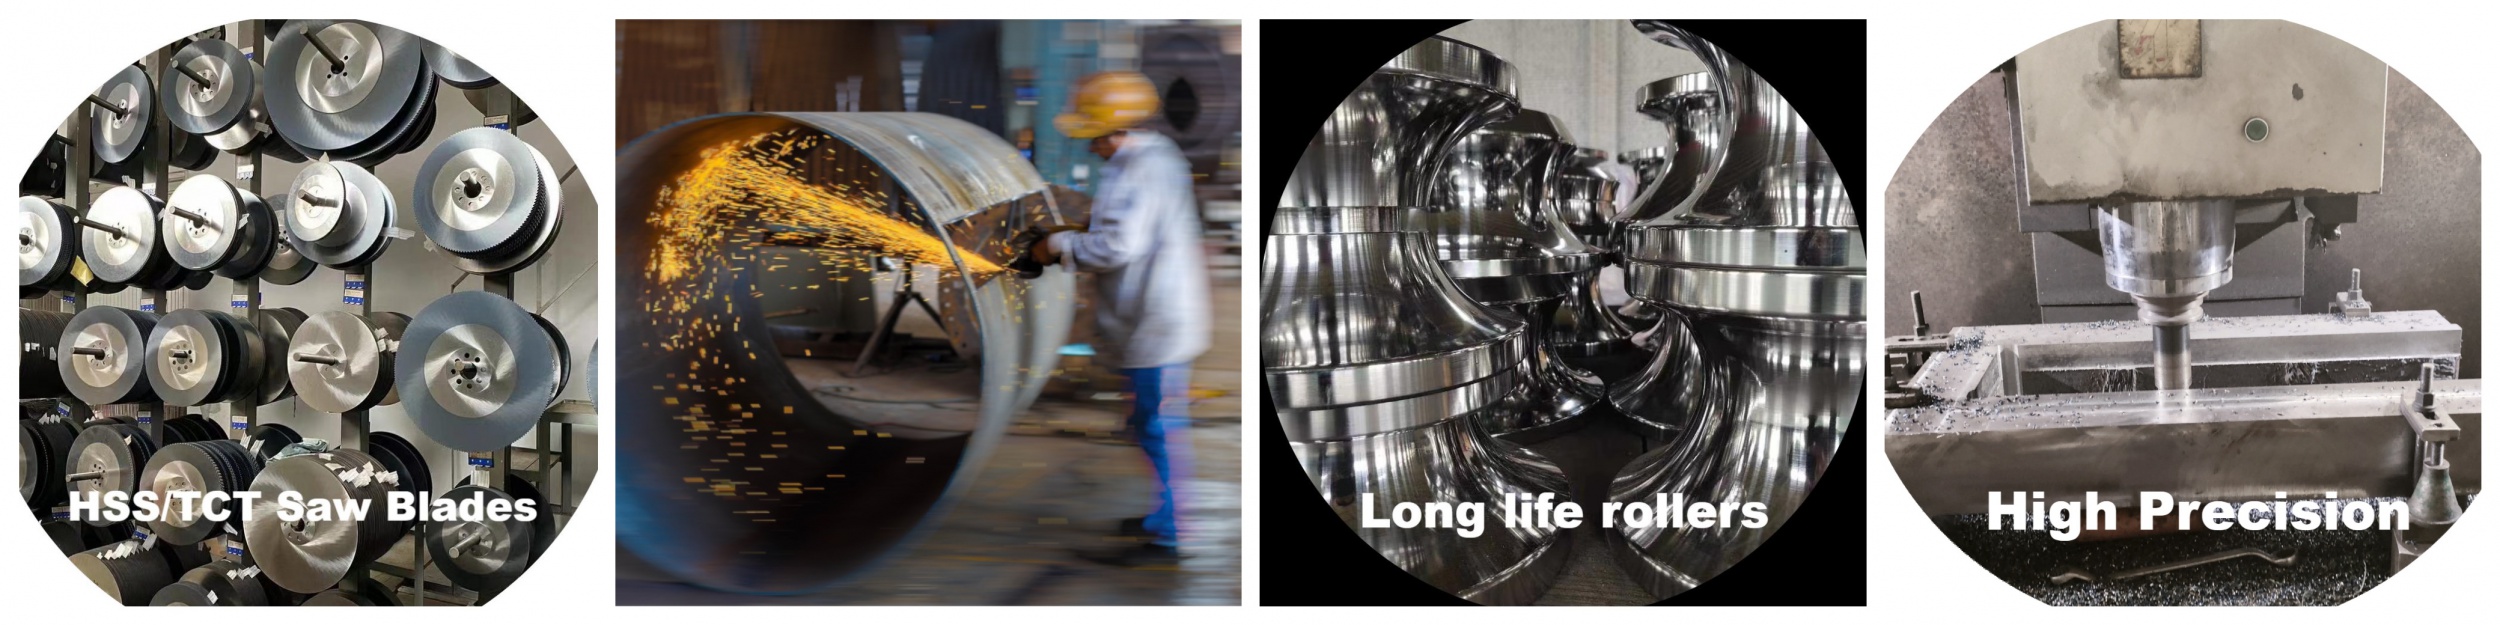
High precision wear resisting and Long life of rollers.
All the machine Lathes, Key Grooves are positioned and Milled by CNC.

Our Machine produce:
a. Round pipe
b. Square and rectangle pipe
c. API standard casing and tubing
d. Solar field pipe
e. Cold forming C,Z,L,U


前 : China ERW 76mm Tube Mill factory and manufacturers
次 : 114mm tube forming machine Tube Mill Line


 製品リンクをコピー
 保存/共有するには画像を長押しします
問い合わせ
問い合わせ

電話番号/Whatsapp/Wechat番号
0086-151-76910262
電子メールアドレス
Linda@aismachinery.com
電話番号/Whatsapp/Wechat番号
0086-151-76910262
電子メールアドレス
Mia@aismachinery.com
 会社住所:RM2401, NO.6 BUILDING, BEIJUN COMMUNITY, NO.370 ZHONGHUA STREET, SHIJIAZHUANG CHINA
暂无链接
Copyright By © AIS Machinery-2020
情報の送信
お問い合わせ

点击右上角
分享给朋友吧


